Precision Metal Stamping Defect Prevention: Root Causes & DFM Solutions
A practical engineering guide detailing root causes and tooling countermeasures for common metal stamping defects: burrs, springback, wrinkling, and distortion.
Precise punch-to-die clearance matching (5%–12% of material thickness) reduces shearing burrs and extends tool life up to 300%.
Overbending geometry and bottoming coining relieve residual elastic strain in high-strength spring alloys (65Mn / SUS301).
TiCN and DLC punch surface coatings eliminate galling and ensure mirror-finish shearing on precision electronic terminals.
1. The 4 Most Common Metal Stamping Defects & Solutions
During mass production of precision stamped brackets, clips, and terminals, process variations can generate visible defects. Below are the engineering root causes and practical toolroom countermeasures:
Excessive Shearing Burrs (冲切毛刺过大)
Root Cause: Cutting clearance between punch and die matrix is too large, uneven, or punch cutting edges have become dull through micro-chipping.
Engineering Countermeasure: Re-grind cutting edges with micro-radius control; adjust punch-die clearance based on material type (5%–8% for copper/brass, 10%–12% for stainless steel); apply TiCN coating to increase punch wear resistance.
Angular Springback in Bending (折弯角度回弹)
Root Cause: Elastic recovery after press stroke release, particularly intense in high-yield spring steels (65Mn, SUS301) and phosphor bronze alloys.
Engineering Countermeasure: Implement 1°–3° overbending in die CAD; incorporate bottoming/coining steps to induce plastic deformation at the bend apex; align primary bend lines perpendicular to sheet rolling grain.
Deep Drawing Wrinkling & Tearing (拉深起皱与破裂)
Root Cause: Wrinkling is caused by insufficient blank holder force causing flange instability; tearing occurs when blank holding force is excessive or die draw radius is too sharp.
Engineering Countermeasure: Use precision nitrogen gas springs for uniform blank holder pressure; optimize draw die shoulder radius (R = 4 to 8 × Thickness); apply specialized extreme-pressure drawing lubricants.
Twisting & Flatness Warpage (零件扭曲与平面度超差)
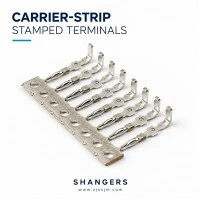
Root Cause: Asymmetric carrier strip tension or internal residual stress released during sequential punching and coining.
Engineering Countermeasure: Add counter-stress leveling stations inside the progressive die layout; balance strip layout with symmetrical pilot locating pins.
2. Quality Control & Tolerance Standard Matrix
How high-precision stamping manufacturers inspect and control critical tolerances during automated mass production:
3. DFM Best Practices to Eliminate Defects at CAD Stage
Early engineering intervention prevents expensive tool re-works. Keep these critical DFM rules in mind when designing stamped hardware:
Placing pierced holes too close to edges causes material bulging and punch deflection. Always maintain at least 2.0x material thickness.
Incorporate rectangular or round bend reliefs next to flanges to prevent tearing and distortion along adjacent flat surfaces.
Avoid sharp 90° corners on external blank profiles. Sharp corners act as stress concentrators and accelerate punch chipping.
📌 Engineering Conclusion
Zero-defect metal stamping is not an accident-it is the result of synchronized DFM component design, precision die engineering, and disciplined in-process quality control. By pairing optimized tooling clearances with proactive springback compensation, manufacturers can reliably achieve aerospace and electrical grade tolerances on high-speed progressive lines.